Steer Tube
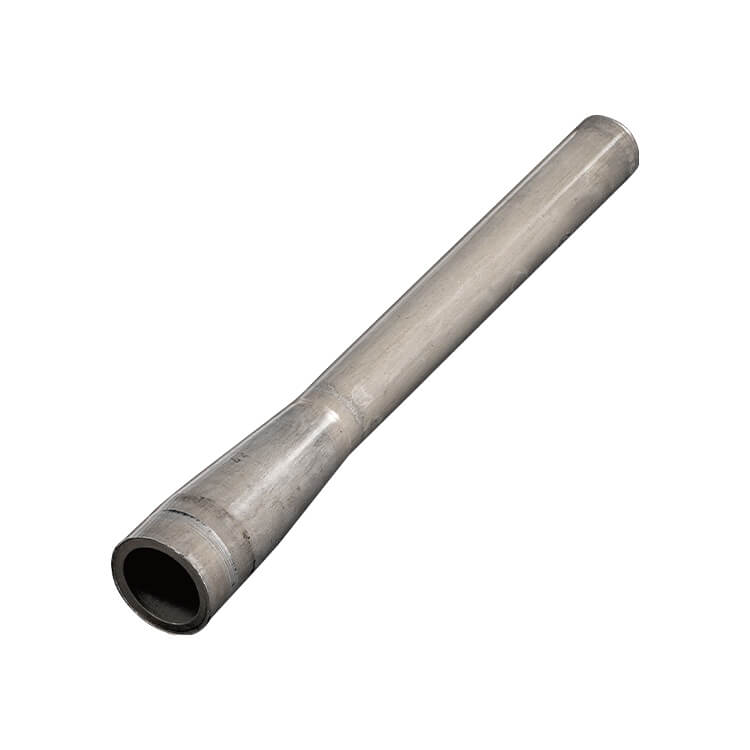
Aluminum Bicycle Steerer Tube: Variable-Diameter Fork Steerer
The aluminum bicycle steerer tube is the steering column of a fork. Its upper end passes through the frame’s head tube and is clamped by the stem, while its lower end joins the fork crown. This version is a long slender tube with a change in outer diameter and a thickened lower section for press-fitting or joining to the crown and for carrying bending loads from steering and braking; variable-diameter designs are also common in tapered head tube systems with different upper and lower bearing sizes.
The joint between steerer and crown sees the highest bending stress and needs a thicker wall, while the upper section can use a thinner wall to save weight. Al Forge Tech (AFT) evaluates cold forming for the diameter change and wall thickness, finish-turns the outer diameter and joint section, and inspects diameter, roundness and straightness on CMM. Anodizing is available.
主要功能
- Thickened, stepped lower section strengthens the crown joint
- Thin-wall upper section saves weight
- OD, roundness and straightness finish-turned and measured
- Can be developed together with the triple clamp
Aluminum Bicycle Steerer Tube Specifications and Manufacturing Capability
| 商品 | 詳細 |
|---|---|
| 產品類別 | Aluminum Forging Bicycle Parts |
| 申請 | Fork steerer tubes for bicycles and e-bikes |
| 主要過程 | Cold forming (cold forging presses 260T–2,500T), evaluated by diameter change and wall thickness |
| 材質 | Selected to customer specification; 2xxx, 5xxx, 6xxx and 7xxx series aluminum alloys available (e.g. 2014, 6061, 6082, 7075) |
| 熱處理 | 根據合金與強度要求而提供的內部 T4 處理方案(8 套)及 T6 人工老化處理方案(7 套) |
| 二次加工 | CNC 加工(52 台加工中心、30 台銑床)、銑削、振動磨削 |
| 表面處理 | 按要求進行陽極氧化(包括硬陽極氧化)、噴射粉碎、電子塗層或塗漆。 |
| 檢查 | Zeiss CMM (4 units), hardness testers, spectrometer, fluorescent penetrant inspection line |
| 尺寸與公差 | 按客戶提供2D/3D圖紙 |
| 品質管理系統 | IATF 16949:2016、ISO 14001:2015 |
Aluminum Bicycle Steerer Tube Manufacturing Process
- 繪圖評估與 DFM我們確認合金、載荷方向和關鍵尺寸,然後執行 QForm 模擬,以預測金屬流動和缺陷風險。.
- 設計與製造銑刀組數(例如,阻斷刀和完成刀)視零件的複雜程度而定,銑刀輪廓則使用便攜式3D掃描儀進行檢查。.
- Cold forging: cold forming on 260T–2,500T presses, suited to thin-walled, tubular and dimensionally repeatable parts.
- 熱處理T4 溶液處理和 T6 人工老化處理均在廠內進行,參數由合金和強度要求設定。.
- CNC加工 以及完成孔、螺紋和接合面均經過機械加工,然後根據需要進行拋光、振動拋光、噴丸或陽極氧化處理。.
- 檢查與運輸尺寸、硬度及化學成分均通過 CMM、硬度測試儀及分光光度儀進行驗證,且所有批次的產品均遵照 IATF 16949 的標準進行追蹤。.
