Upper Metal-1
Description
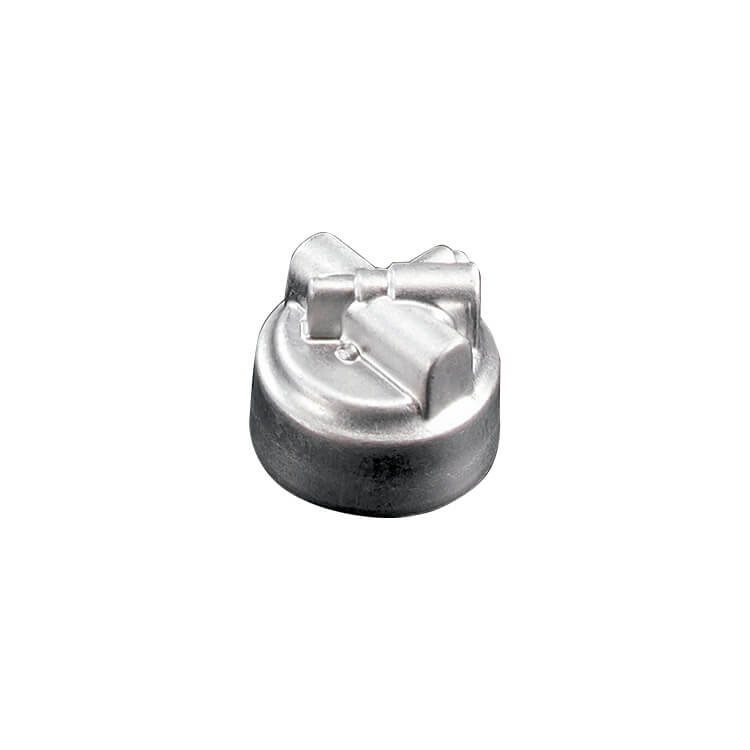
Forged Aluminum Shock Upper Mount: Suspension Joint Seat
The forged aluminum shock upper mount is the joint seat at the top of a shock absorber. It combines a cylindrical base with a flat connecting ear above it; the ear is machined with a mounting hole to fix it to the frame or suspension link, while the cylindrical base joins the shock body. Suspension joints like this carry both the shock’s axial force and impacts transmitted from the chassis.
The transition between ear and base is a stress concentration. Al Forge Tech (AFT) hot forges the part so grain flow runs continuously from base to ear, and raises strength with in-house T6 heat treatment. Mounting holes, threads and mating faces are then machined, with anodizing available, so the part can ship ready for assembly.
Key Features
- Cylindrical base and ear hot forged in one piece with continuous grain flow
- Mounting hole, thread and shock mating faces machinable
- In-house T6 heat treatment for strength
- Anodizing for corrosion resistance and appearance
Forged Aluminum Shock Upper Mount Specifications and Manufacturing Capability
| Item | Details |
|---|---|
| Product category | Aluminum Forging Industrial Hardware |
| Application | Shock absorber upper joints, suspension link joint seats |
| Primary process | Closed-die hot forging (hot forging presses 600T–8,000T) |
| Material | Selected to customer specification; 2xxx, 5xxx, 6xxx and 7xxx series aluminum alloys available (e.g. 2014, 6061, 6082, 7075) |
| Heat treatment | In-house T4 solution treatment (8 units) and T6 artificial aging (7 units), set by alloy and strength requirement |
| Secondary machining | CNC machining (52 machining centers, 30 lathes), deburring, vibratory finishing |
| Surface finish | Anodizing (including hard anodizing), shot blasting, e-coating or painting, as required |
| Inspection | Zeiss CMM (4 units), hardness testers, spectrometer, fluorescent penetrant inspection line |
| Dimensions and tolerances | Per customer 2D/3D drawings |
| Quality system | IATF 16949:2016, ISO 14001:2015 |
Forged Aluminum Shock Upper Mount Manufacturing Process
- Drawing review and DFM: we confirm alloy, load direction and critical dimensions, then run QForm simulation to predict metal flow and defect risk.
- Die design and manufacturing: the number of die sets (for example, blocker and finisher dies) is planned around part complexity, and die contours are checked with a portable 3D scanner.
- Hot forging: closed-die forming on 600T–8,000T hot forging presses creates a continuous grain flow that follows the part contour.
- Heat treatment: T4 solution treatment and T6 artificial aging are performed in-house, with parameters set by alloy and strength requirement.
- CNC machining and finishing: holes, threads and mating surfaces are machined, followed by deburring, vibratory finishing, shot blasting or anodizing as required.
- Inspection and shipment: dimensions, hardness and chemical composition are verified with CMM, hardness testers and a spectrometer, with lot traceability kept under IATF 16949.
FAQ
Which aluminum alloys are typical for a shock upper mount?
Selection depends on strength, corrosion and machining needs. AFT works with 2xxx, 5xxx, 6xxx and 7xxx series alloys; 6xxx grades common in chassis and suspension parts include 6061, 6082 and 6110, and 7xxx grades can be evaluated for higher strength. The final alloy is confirmed against your drawing specification and load conditions.
How is mounting hole accuracy controlled?
Mounting holes and mating faces are CNC-machined after T6 heat treatment so heat-treatment distortion does not affect hole position. AFT machines holes, threads and mating faces from a common datum and measures diameter, position and perpendicularity on Zeiss CMM to ensure the fit with bushings or bolts meets the drawing.
Is heat treatment for the Forged Aluminum Shock Upper Mount done in-house?
Yes. Al Forge Tech operates 8 T4 solution treatment units and 7 T6 artificial aging units on site, so the Forged Aluminum Shock Upper Mount can be solution treated, quenched and aged in the same facility before machining and inspection. Keeping heat treatment in-house removes inter-plant transport, reduces lead-time risk and keeps lot traceability within one quality system. Parameters are set according to the alloy grade and your specification.
Can you assess forging feasibility while the Forged Aluminum Shock Upper Mount is still in design?
Yes. Al Forge Tech works mainly as an OEM supplier, and our engineers can give design-for-manufacturability (DFM) feedback at the concept or drawing stage, such as adjusting thin ribs, abrupt section changes or draft angles to avoid laps and underfill. QForm simulation predicts metal flow early, and the results are cross-checked against our die design experience.
How are MOQ and lead time for the Forged Aluminum Shock Upper Mount determined?
MOQ and lead time depend on part size, number of die sets, alloy and machining scope, and are confirmed in the quotation after drawing review. The typical sequence is die development, forged samples, sample approval and then mass production. Sharing your annual volume and call-off schedule helps us plan dies and capacity for the Forged Aluminum Shock Upper Mount.
Request a Quote for the Forged Aluminum Shock Upper Mount
Developing a new Forged Aluminum Shock Upper Mount or converting an existing part to aluminum forging? Send us your 3D/2D drawings, alloy and temper, annual volume and finishing requirements. Our engineering team will reply with a feasibility review, die plan and quotation.
- Online inquiry: Contact Us
- Email: [email protected]
To compare similar parts, browse Aluminum Forging Industrial Hardware and our industrial hardware forging applications, or visit About Us for our equipment and certifications.
