Suspension Body-1
説明
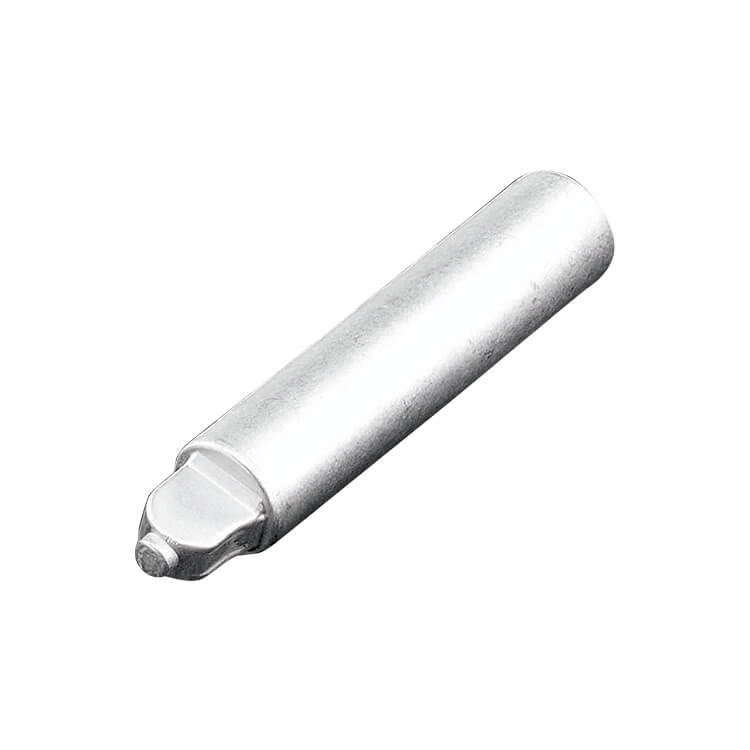
Aluminum Suspension Body: Shock Body with Closed End and Boss
The aluminum suspension body is the main body of a rear shock absorber: a long round tube with one open end and a closed end featuring a tapered transition and a small-diameter boss, which can be machined into a mounting shaft or connector. Body and closed end are formed in one piece and are used in rear suspension systems for motorcycles, bicycles and ATVs.
Al Forge Tech (AFT) cold impact extrudes the body and closed end so there is no weld between wall and end and the grain flow stays continuous. The bore, boss and faces can then be turned in-house, threads or mounting holes machined, and the part anodized for wear resistance and appearance. For high-strength bodies, T6 heat treatment conditions are selected according to alloy.
主な機能
- Body, closed end and boss formed in one piece, no weld
- Tapered transition reduces stress concentration at the end
- Boss machinable into a mounting shaft, thread or connector
- Bore finishing with anodizing or hard anodizing
Aluminum Suspension Body Specifications and Manufacturing Capability
| 商品 | 詳細 |
|---|---|
| 製品カテゴリー | アルミ鍛造工業用金物 |
| 申請 | Rear shock bodies for motorcycles, bicycles and ATVs |
| 主なプロセス | Cold impact extrusion (cold forging presses 260T–2,500T) |
| 素材 | お客様の仕様に合わせて選択可能。2xxx、5xxx、6xxx、7xxx シリーズのアルミニウム合金(例:2014、6061、6082、7075) |
| 熱処理 | 合金および強度要件による社内T4処理(8ユニット)およびT6人工老化(7ユニット) |
| 二次加工 | CNC加工(52台の加工センター、30台の旋盤)、バリ取り、振動仕上げ |
| 表面仕上げ | 必要に応じて、陽極酸化(硬陽極酸化を含む)、ショットブラスト、電子コーティングまたは塗装 |
| 検査 | ザイツCMM(4台)、硬度計、分光計、蛍光透過検査ライン |
| 寸法と公差 | 顧客ごとに2D/3D図面 |
| 品質システム | IATF 16949:2016、ISO 14001:2015 |
Aluminum Suspension Body Manufacturing Process
- ドローイングレビューとDFM合金、荷重方向、重要な寸法を確認し、その後 QForm シミュレーションを実行して金属流動と欠陥リスクを予測します。.
- デザインと製造ダイセットの数(例えば、ブロッカーダイとファイニッシャーダイ)は部品の複雑さに合わせて計画されており、ダイの形状は携帯型3Dスキャナーで確認されます。.
- Cold forging:impact extrusion on 260T–2,500T presses, suited to thin-walled, tubular and dimensionally repeatable parts.
- 熱処理T4溶液処理とT6人工老化は社内で実施され、合金および強度要件によって設定されたパラメータが使用されます。.
- CNC加工 そして仕上げ穴、スレッド、接合面は機械加工され、その後、必要に応じてバリ取り、振動仕上げ、ショットブラスト、または陽極酸化が行われます。.
- 検査と発送寸法、硬度、化学組成はCMM、硬度計、分光計を用いて確認され、ロットのトレーサビリティはIATF 16949に従って管理されています。.
よくある質問
How is the boss on the closed end formed?
The closed end and boss can be formed together with the body during impact extrusion, or the closed-end body can be formed first and the boss completed by a further forging or machining step. The approach depends on boss size and wall thickness. AFT evaluates one-shot feasibility at drawing review and explains any staged tooling and machining in the quotation.
How does a rear suspension body differ in process from a fork inner tube?
A rear suspension body is usually a closed-end shell that must hold the damper’s internal oil and gas pressure, so wall uniformity and end strength matter most. A fork inner tube is primarily a sliding surface, so OD accuracy, surface treatment and straightness matter most. Both can be produced from impact extrusion or extruded tube, and AFT recommends the process by design and volume.
How do you keep the Aluminum Suspension Body consistent from lot to lot?
Al Forge Tech runs incoming (IQC), in-process (IPQC) and final (FQC) inspection under IATF 16949:2016, supported by 4 Zeiss CMMs, hardness testers, a spectrometer and a fluorescent penetrant inspection line. First, middle and last pieces of every lot are checked against the die; when wear causes dimensional drift, the die is reworked to keep the Aluminum Suspension Body stable across lots.
Is heat treatment for the Aluminum Suspension Body done in-house?
Yes. Al Forge Tech operates 8 T4 solution treatment units and 7 T6 artificial aging units on site, so the Aluminum Suspension Body can be solution treated, quenched and aged in the same facility before machining and inspection. Keeping heat treatment in-house removes inter-plant transport, reduces lead-time risk and keeps lot traceability within one quality system. Parameters are set according to the alloy grade and your specification.
How does a forged aluminum Aluminum Suspension Body compare with casting or machining from billet?
Forging shapes aluminum in the solid state under pressure, so the grain flow follows the part contour and the porosity and shrinkage common in castings are avoided. Compared with machining from solid billet, a near-net-shape forging removes less material and shortens machining time. For a Aluminum Suspension Body under repeated loads, forging balances strength and weight; the final choice still depends on design loads and volume.
Request a Quote for the Aluminum Suspension Body
Developing a new Aluminum Suspension Body or converting an existing part to aluminum forging? Send us your 3D/2D drawings, alloy and temper, annual volume and finishing requirements. Our engineering team will reply with a feasibility review, die plan and quotation.
- オンラインのお問い合わせ: お問い合わせ
- メールアドレス: [email protected]
類似のパーツを比較するには、閲覧してください。 アルミ鍛造工業用金物 そして私たちの industrial hardware forging applications, または、こちらをご覧ください 会社紹介 当社の設備および認証について。.
