Rear Supporting Bracket
説明
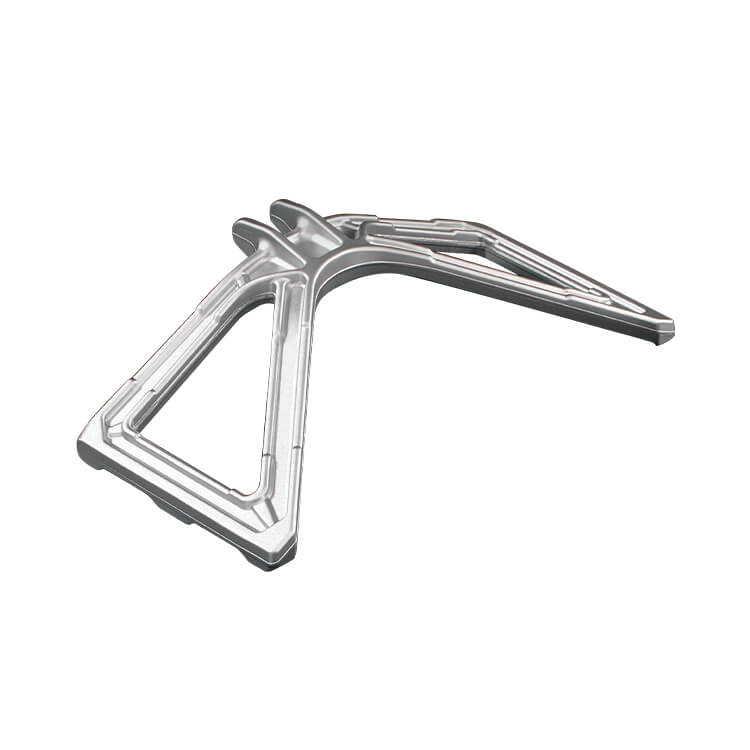
Forged Aluminum Rear Supporting Bracket: Snowmobile Rear Suspension Bracket
The forged aluminum rear supporting bracket is a structural bracket in a snowmobile’s rear suspension. It is a truss made of a triangular frame and an extended arm, with an open frame to save weight and mounting bosses at each end that connect to the rear suspension rails, shock absorber and chassis. The bracket is forged in one piece, replacing a multi-part welded assembly.
Snowmobiles run in cold, high-impact conditions, so the rear bracket must carry repeated impacts and torsional loads from the snow surface. Al Forge Tech (AFT) closed-die hot forges the bracket so grain flow runs continuously along the frame members, avoiding the heat-affected weakening at welded joints, and finishes mounting holes and mating faces after in-house T6 heat treatment and CNC machining.
主な機能
- Triangular truss forged in one piece, replacing welded assemblies
- Open-frame design balances rigidity and weight
- All mounting points CNC-machined and CMM-checked
- Suited to cold, high-impact snowmobile rear suspension
Forged Aluminum Rear Supporting Bracket Specifications and Manufacturing Capability
| 商品 | 詳細 |
|---|---|
| 製品カテゴリー | 特殊車両部品 |
| 申請 | Snowmobile rear suspension systems, structural brackets for powersport vehicles |
| 主なプロセス | 閉型熱間鍛造(熱間鍛造プレス:600T~8,000T) |
| 素材 | Per customer specification; 6xxx alloys common for chassis and suspension parts (e.g. 6061, 6082, 6110), 7xxx evaluated for higher strength |
| 熱処理 | 合金および強度要件による社内T4処理(8ユニット)およびT6人工老化(7ユニット) |
| 二次加工 | CNC加工(52台の加工センター、30台の旋盤)、バリ取り、振動仕上げ |
| 表面仕上げ | 必要に応じて、陽極酸化(硬陽極酸化を含む)、ショットブラスト、電子コーティングまたは塗装 |
| 検査 | Zeiss CMM (4 units), hardness testers, spectrometer, fluorescent penetrant line; tensile and fatigue testing available |
| 寸法と公差 | 顧客ごとに2D/3D図面 |
| 品質システム | IATF 16949:2016、ISO 14001:2015 |
Forged Aluminum Rear Supporting Bracket Manufacturing Process
- ドローイングレビューとDFM合金、荷重方向、重要な寸法を確認し、その後 QForm シミュレーションを実行して金属流動と欠陥リスクを予測します。.
- デザインと製造ダイセットの数(例えば、ブロッカーダイとファイニッシャーダイ)は部品の複雑さに合わせて計画されており、ダイの形状は携帯型3Dスキャナーで確認されます。.
- 熱間鍛造600T~8,000Tの熱間鍛造プレスでの閉型成形により、部品の形状に沿った連続した粒状流が生成されます。.
- 熱処理T4溶液処理とT6人工老化は社内で実施され、合金および強度要件によって設定されたパラメータが使用されます。.
- CNC加工 そして仕上げ穴、スレッド、接合面は機械加工され、その後、必要に応じてバリ取り、振動仕上げ、ショットブラスト、または陽極酸化が行われます。.
- 検査と発送寸法、硬度、化学組成はCMM、硬度計、分光計を用いて確認され、ロットのトレーサビリティはIATF 16949に従って管理されています。.
よくある質問
Why replace a welded snowmobile bracket with a forging?
A welded bracket is assembled from several profiles or tubes, and the weld and heat-affected zone are usually weaker than the base metal, making them likely fatigue-crack initiation sites under repeated impact. A forged bracket is a single piece without welded joints, with grain flow continuous along the members. It also eliminates assembly steps and fixtures and makes dimensional consistency easier to hold in production.
How are distortion and hole accuracy controlled on a large frame forging?
Frame forgings can distort during quenching because of uneven sections. AFT balances member sections during die and process design, straightens after heat treatment, and CNC-machines the mounting holes afterward so heat-treatment distortion does not affect hole positions. Hole positions and flatness are then measured on Zeiss CMM.
How does a forged aluminum Forged Aluminum Rear Supporting Bracket compare with casting or machining from billet?
Forging shapes aluminum in the solid state under pressure, so the grain flow follows the part contour and the porosity and shrinkage common in castings are avoided. Compared with machining from solid billet, a near-net-shape forging removes less material and shortens machining time. For a Forged Aluminum Rear Supporting Bracket under repeated loads, forging balances strength and weight; the final choice still depends on design loads and volume.
How do you keep the Forged Aluminum Rear Supporting Bracket consistent from lot to lot?
Al Forge Tech runs incoming (IQC), in-process (IPQC) and final (FQC) inspection under IATF 16949:2016, supported by 4 Zeiss CMMs, hardness testers, a spectrometer and a fluorescent penetrant inspection line. First, middle and last pieces of every lot are checked against the die; when wear causes dimensional drift, the die is reworked to keep the Forged Aluminum Rear Supporting Bracket stable across lots.
How are MOQ and lead time for the Forged Aluminum Rear Supporting Bracket determined?
MOQ and lead time depend on part size, number of die sets, alloy and machining scope, and are confirmed in the quotation after drawing review. The typical sequence is die development, forged samples, sample approval and then mass production. Sharing your annual volume and call-off schedule helps us plan dies and capacity for the Forged Aluminum Rear Supporting Bracket.
Request a Quote for the Forged Aluminum Rear Supporting Bracket
Developing a new Forged Aluminum Rear Supporting Bracket or converting an existing part to aluminum forging? Send us your 3D/2D drawings, alloy and temper, annual volume and finishing requirements. Our engineering team will reply with a feasibility review, die plan and quotation.
- オンラインのお問い合わせ: お問い合わせ
- メールアドレス: [email protected]
類似のパーツを比較するには、閲覧してください。 特殊車両部品 そして私たちの 自動車用アルミニウム鍛造用途, または、こちらをご覧ください 会社紹介 当社の設備および認証について。.
