Ratchet
Description
Forged Aluminum Bicycle Ratchet: Externally Splined Barrel Drive Part
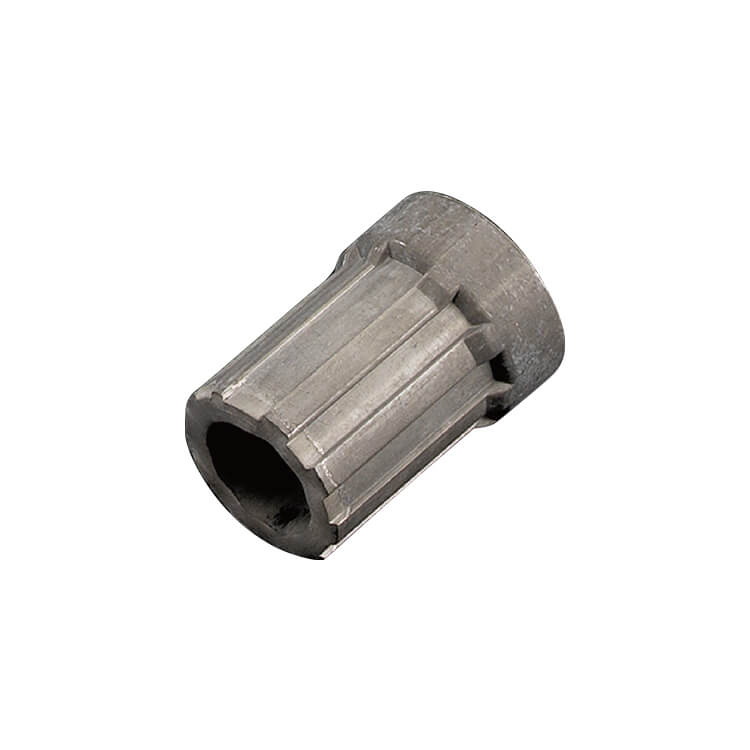
The forged aluminum bicycle ratchet is a barrel-shaped drive part for bicycle hubs or drivetrains. It is a cylindrical body with multiple axial spline teeth around its outside and a larger-diameter flange ring at one end. The external splines mate with cassette sprockets or cogs to transmit torque, while the flange ring acts as an axial locating face or pawl engagement surface.
Machining external splines requires milling or hobbing; forging the splines to near-net shape shortens machining and keeps grain flow following the tooth form. Al Forge Tech (AFT) evaluates cold or hot forging by spline accuracy and wall thickness, finish-turns and CNC-finishes the diameters and splines after heat treatment, and offers hard anodizing for wear-resistant tooth faces.
Key Features
- External-spline barrel and flange ring formed in one piece
- Near-net splines shorten milling or hobbing time
- Diameters and splines turned and CNC-finished
- Hard anodizing for wear-resistant tooth faces
Forged Aluminum Bicycle Ratchet Specifications and Manufacturing Capability
| Item | Details |
|---|---|
| Product category | Aluminum Forging Bicycle Parts |
| Application | Bicycle hubs (e.g. freehub bodies), ratchets and drivetrains |
| Primary process | Hot or cold forging, selected by spline accuracy and wall thickness (hot 600T–8,000T / cold 260T–2,500T) |
| Material | Selected to customer specification; 2xxx, 5xxx, 6xxx and 7xxx series aluminum alloys available (e.g. 2014, 6061, 6082, 7075) |
| Heat treatment | In-house T4 solution treatment (8 units) and T6 artificial aging (7 units), set by alloy and strength requirement |
| Secondary machining | CNC machining (52 machining centers, 30 lathes), deburring, vibratory finishing |
| Surface finish | Anodizing (including hard anodizing), shot blasting, e-coating or painting, as required |
| Inspection | Zeiss CMM (4 units), hardness testers, spectrometer, fluorescent penetrant inspection line |
| Dimensions and tolerances | Per customer 2D/3D drawings |
| Quality system | IATF 16949:2016, ISO 14001:2015 |
Forged Aluminum Bicycle Ratchet Manufacturing Process
- Drawing review and DFM: we confirm alloy, load direction and critical dimensions, then run QForm simulation to predict metal flow and defect risk.
- Die design and manufacturing: the number of die sets (for example, blocker and finisher dies) is planned around part complexity, and die contours are checked with a portable 3D scanner.
- Cold forging: cold forming on 260T–2,500T presses, suited to thin-walled, tubular and dimensionally repeatable parts.
- Heat treatment: T4 solution treatment and T6 artificial aging are performed in-house, with parameters set by alloy and strength requirement.
- CNC machining and finishing: holes, threads and mating surfaces are machined, followed by deburring, vibratory finishing, shot blasting or anodizing as required.
- Inspection and shipment: dimensions, hardness and chemical composition are verified with CMM, hardness testers and a spectrometer, with lot traceability kept under IATF 16949.
FAQ
How do I choose between an aluminum and a steel ratchet?
An aluminum ratchet is lighter and suits weight-focused hub and drivetrain designs, but its tooth surface is softer than steel, so hard anodizing and controlled contact pressure are usually needed. A steel ratchet is more wear-resistant and suits high-load or long-life designs. The material should be evaluated against the mating parts and loads; AFT focuses on aluminum forging solutions.
How is the external spline fit with the cassette ensured?
Spline profile, tooth thickness and measurement over pins determine how tightly the cassette fits. AFT forges near-net splines, finishes them to tolerance after heat treatment and measures tooth form and OD with CMM, a profile meter and gauges. If hard anodizing follows, machining dimensions allow for film thickness so the treated part still meets the fit tolerance.
Can the Forged Aluminum Bicycle Ratchet be anodized or given other surface finishes?
Yes. Al Forge Tech offers anodizing (including hard anodizing), shot blasting, vibratory finishing, e-coating and painting, plus pickling and ultrasonic washing lines to clean parts after machining. Please note the finish type and film thickness on the drawing so machining allowances and cosmetic standards for the Forged Aluminum Bicycle Ratchet can be evaluated together.
How do you keep the Forged Aluminum Bicycle Ratchet consistent from lot to lot?
Al Forge Tech runs incoming (IQC), in-process (IPQC) and final (FQC) inspection under IATF 16949:2016, supported by 4 Zeiss CMMs, hardness testers, a spectrometer and a fluorescent penetrant inspection line. First, middle and last pieces of every lot are checked against the die; when wear causes dimensional drift, the die is reworked to keep the Forged Aluminum Bicycle Ratchet stable across lots.
What information do you need to quote the Forged Aluminum Bicycle Ratchet?
Please send a 3D model and 2D drawing, alloy grade and temper, critical tolerances, surface finish requirements, estimated annual volume and target delivery date. Complete data lets our engineers judge forging feasibility, the number of die sets and the machining scope for the Forged Aluminum Bicycle Ratchet at the quotation stage. If the design is still conceptual, a sketch is enough to start a DFM discussion.
Request a Quote for the Forged Aluminum Bicycle Ratchet
Developing a new Forged Aluminum Bicycle Ratchet or converting an existing part to aluminum forging? Send us your 3D/2D drawings, alloy and temper, annual volume and finishing requirements. Our engineering team will reply with a feasibility review, die plan and quotation.
- Online inquiry: Contact Us
- Email: [email protected]
To compare similar parts, browse Aluminum Forging Bicycle Parts and our automotive aluminum forging applications, or visit About Us for our equipment and certifications.
