Impact Extrusion Tube-4
Description
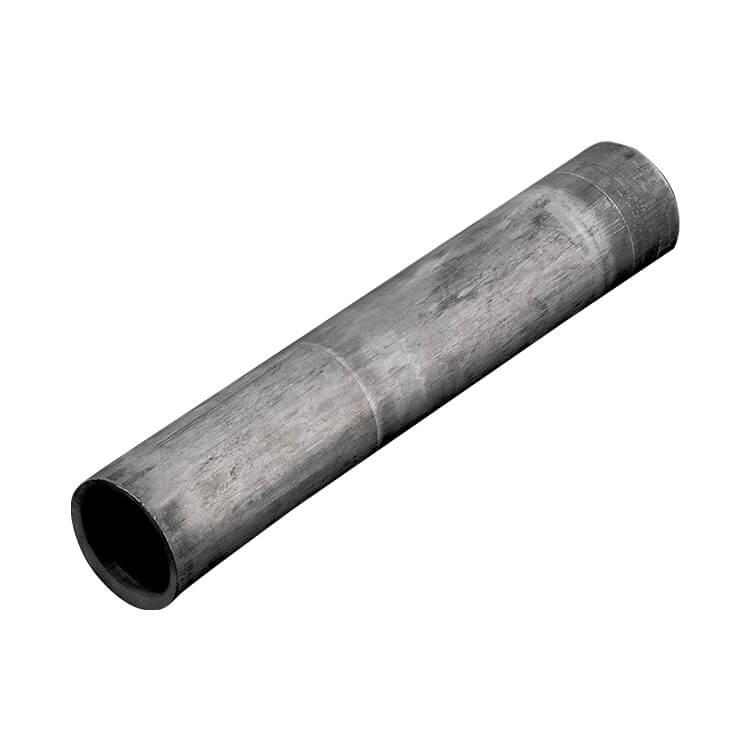
Aluminum Long Impact Extrusion Tube: Long Thin-Wall Tube with Stepped Sections
The aluminum long impact extrusion tube is a longer thin-walled round tube with a diameter step along its body. Al Forge Tech (AFT) cold impact extrudes the tube body and then machines the ends and stepped sections to drawing. Long tubes like this are common as shock absorber outer tubes, hydraulic or pneumatic cylinder barrels, telescopic outer tubes and long protective sleeves.
Long tubes demand even wall thickness and good straightness. In impact extrusion, metal flow is governed by the gap between punch and die, giving a stable wall-thickness distribution. AFT plans the forming sequence by length and wall thickness, then straightens after heat treatment, faces the ends and inspects dimensions, with anodizing available for wear and corrosion resistance.
Key Features
- Long thin-wall body cold formed with stable wall thickness
- Stepped outer diameters designed to suit mating parts
- Straightening and straightness inspection after heat treatment
- Anodizing or hard anodizing for wear resistance
Aluminum Long Impact Extrusion Tube Specifications and Manufacturing Capability
| Item | Details |
|---|---|
| Product category | Aluminum Forging Industrial Hardware |
| Application | Shock absorber outer tubes, hydraulic/pneumatic cylinder barrels, telescopic outer tubes, long protective sleeves |
| Primary process | Cold impact extrusion (cold forging presses 260T–2,500T) |
| Material | Selected to customer specification; 2xxx, 5xxx, 6xxx and 7xxx series aluminum alloys available (e.g. 2014, 6061, 6082, 7075) |
| Heat treatment | In-house T4 solution treatment (8 units) and T6 artificial aging (7 units), set by alloy and strength requirement |
| Secondary machining | CNC machining (52 machining centers, 30 lathes), deburring, vibratory finishing |
| Surface finish | Anodizing (including hard anodizing), shot blasting, e-coating or painting, as required |
| Inspection | Zeiss CMM (4 units), hardness testers, spectrometer, fluorescent penetrant inspection line |
| Dimensions and tolerances | Per customer 2D/3D drawings |
| Quality system | IATF 16949:2016, ISO 14001:2015 |
Aluminum Long Impact Extrusion Tube Manufacturing Process
- Drawing review and DFM: we confirm alloy, load direction and critical dimensions, then run QForm simulation to predict metal flow and defect risk.
- Die design and manufacturing: the number of die sets (for example, blocker and finisher dies) is planned around part complexity, and die contours are checked with a portable 3D scanner.
- Cold forging: impact extrusion on 260T–2,500T presses, suited to thin-walled, tubular and dimensionally repeatable parts.
- Heat treatment: T4 solution treatment and T6 artificial aging are performed in-house, with parameters set by alloy and strength requirement.
- CNC machining and finishing: holes, threads and mating surfaces are machined, followed by deburring, vibratory finishing, shot blasting or anodizing as required.
- Inspection and shipment: dimensions, hardness and chemical composition are verified with CMM, hardness testers and a spectrometer, with lot traceability kept under IATF 16949.
FAQ
How is straightness controlled on a long impact extruded tube?
Straightness is affected by forming, quenching during heat treatment and machining. AFT keeps punch and die concentric in the tool design to limit run-out during forming, straightens after heat treatment where needed, and measures straightness and runout during turning and inspection. Please state the tolerance on the drawing so we can judge whether extra straightening or finishing steps are required.
How does impact extruding a long tube differ from a short one?
A long tube needs a longer stroke and higher forming force, and the thinner and longer the wall, the more carefully metal flow must be controlled to avoid uneven walls or a ragged rim. AFT’s cold forging presses cover 260T–2,500T, and we select the press and decide whether staged forming or trimming of the open end is needed based on diameter, wall thickness and length.
Can the Aluminum Long Impact Extrusion Tube be anodized or given other surface finishes?
Yes. Al Forge Tech offers anodizing (including hard anodizing), shot blasting, vibratory finishing, e-coating and painting, plus pickling and ultrasonic washing lines to clean parts after machining. Please note the finish type and film thickness on the drawing so machining allowances and cosmetic standards for the Aluminum Long Impact Extrusion Tube can be evaluated together.
How are MOQ and lead time for the Aluminum Long Impact Extrusion Tube determined?
MOQ and lead time depend on part size, number of die sets, alloy and machining scope, and are confirmed in the quotation after drawing review. The typical sequence is die development, forged samples, sample approval and then mass production. Sharing your annual volume and call-off schedule helps us plan dies and capacity for the Aluminum Long Impact Extrusion Tube.
Can you assess forging feasibility while the Aluminum Long Impact Extrusion Tube is still in design?
Yes. Al Forge Tech works mainly as an OEM supplier, and our engineers can give design-for-manufacturability (DFM) feedback at the concept or drawing stage, such as adjusting thin ribs, abrupt section changes or draft angles to avoid laps and underfill. QForm simulation predicts metal flow early, and the results are cross-checked against our die design experience.
Request a Quote for the Aluminum Long Impact Extrusion Tube
Developing a new Aluminum Long Impact Extrusion Tube or converting an existing part to aluminum forging? Send us your 3D/2D drawings, alloy and temper, annual volume and finishing requirements. Our engineering team will reply with a feasibility review, die plan and quotation.
- Online inquiry: Contact Us
- Email: [email protected]
To compare similar parts, browse Aluminum Forging Industrial Hardware and our industrial hardware forging applications, or visit About Us for our equipment and certifications.
