Functional Teeth
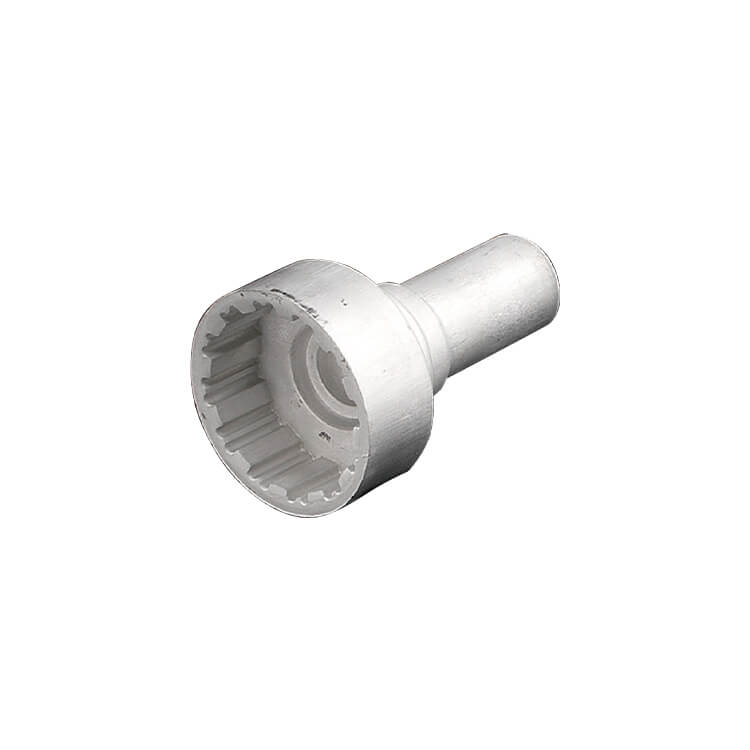
Forged Aluminum Bicycle Toothed Driver: Internally Toothed Cup and Shaft in One Piece
The forged aluminum bicycle toothed driver (functional teeth) is a toothed part for bicycle drivetrain or ratchet mechanisms. It consists of a cup with internal teeth and a cylindrical shaft extending from one end. Grooves are arranged around the inner wall of the cup to engage pawls, splines or mating teeth and transmit torque. Cup and shaft are formed in one piece, reducing fit errors between assembled parts.
Machining internal teeth requires dedicated operations such as gear shaping or broaching, which take time. Forging the tooth grooves to near-net shape first greatly shortens machining and keeps grain flow following the tooth form. Al Forge Tech (AFT) evaluates cold or hot forging by tooth accuracy and wall thickness, has an in-house broaching machine for finishing internal teeth, and inspects tooth form and concentricity with CMM and gauges.
Key Features
- Internally toothed cup and shaft formed in one piece
- Near-net forged teeth shorten shaping or broaching time
- In-house broaching for finishing internal teeth
- Tooth form and concentricity measured on CMM
Forged Aluminum Bicycle Toothed Driver Specifications and Manufacturing Capability
| Item | Details |
|---|---|
| Product category | Aluminum Forging Bicycle Parts |
| Application | Bicycle hub, ratchet and drivetrain toothed parts |
| Primary process | Hot or cold forging, selected by tooth accuracy and wall thickness (hot 600T–8,000T / cold 260T–2,500T) |
| Material | Selected to customer specification; 2xxx, 5xxx, 6xxx and 7xxx series aluminum alloys available (e.g. 2014, 6061, 6082, 7075) |
| Heat treatment | In-house T4 solution treatment (8 units) and T6 artificial aging (7 units), set by alloy and strength requirement |
| Secondary machining | CNC machining (52 machining centers, 30 lathes), deburring, vibratory finishing |
| Surface finish | Anodizing (including hard anodizing), shot blasting, e-coating or painting, as required |
| Inspection | Zeiss CMM (4 units), hardness testers, spectrometer, fluorescent penetrant inspection line |
| Dimensions and tolerances | Per customer 2D/3D drawings |
| Quality system | IATF 16949:2016, ISO 14001:2015 |
Forged Aluminum Bicycle Toothed Driver Manufacturing Process
- Drawing review and DFM: we confirm alloy, load direction and critical dimensions, then run QForm simulation to predict metal flow and defect risk.
- Die design and manufacturing: the number of die sets (for example, blocker and finisher dies) is planned around part complexity, and die contours are checked with a portable 3D scanner.
- Cold forging: cold forming on 260T–2,500T presses, suited to thin-walled, tubular and dimensionally repeatable parts.
- Heat treatment: T4 solution treatment and T6 artificial aging are performed in-house, with parameters set by alloy and strength requirement.
- CNC machining and finishing: holes, threads and mating surfaces are machined, followed by deburring, vibratory finishing, shot blasting or anodizing as required.
- Inspection and shipment: dimensions, hardness and chemical composition are verified with CMM, hardness testers and a spectrometer, with lot traceability kept under IATF 16949.
