Seat Post
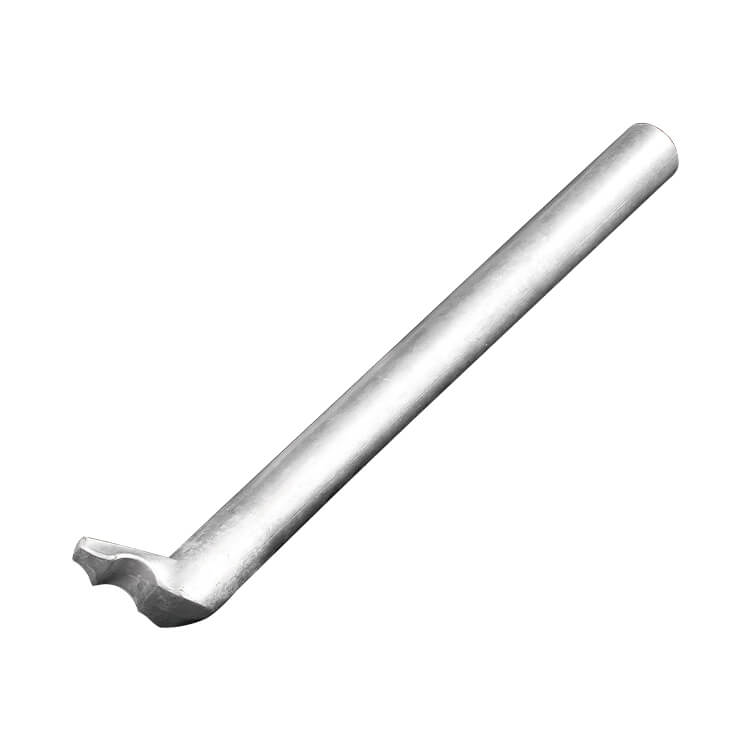
Forged Aluminum Bicycle Seat Post: Shaft and Saddle Clamp Head in One Piece
The forged aluminum bicycle seat post connects the saddle to the frame. It is a long slender tube with a bent saddle clamp head at the top for mounting the saddle rail clamp. A one-piece seat post forms the shaft and clamp head together, with no welded or bolted-on head, giving a simple, light structure.
The bent clamp head carries the bending load from the rider’s weight and is the most heavily stressed area of the post. Al Forge Tech (AFT) forges the head so grain flow turns continuously from shaft into head, avoiding the heat-affected weakening of a welded head. After heat treatment, the clamp bore, threads and shaft diameter are machined, and anodizing or shot blasting can be applied for appearance and corrosion resistance.
Key Features
- Shaft and saddle clamp head formed in one piece, no weld
- Continuous grain flow through the bent head under bending load
- Clamp bore, threads and shaft diameter machined
- Anodized or shot-blasted finish
Forged Aluminum Bicycle Seat Post Specifications and Manufacturing Capability
| Item | Details |
|---|---|
| Product category | Aluminum Forging Bicycle Parts |
| Application | Seat posts for bicycles and e-bikes |
| Primary process | Closed-die hot forging (hot forging presses 600T–8,000T) |
| Material | Selected to customer specification; 2xxx, 5xxx, 6xxx and 7xxx series aluminum alloys available (e.g. 2014, 6061, 6082, 7075) |
| Heat treatment | In-house T4 solution treatment (8 units) and T6 artificial aging (7 units), set by alloy and strength requirement |
| Secondary machining | CNC machining (52 machining centers, 30 lathes), deburring, vibratory finishing |
| Surface finish | Anodizing (including hard anodizing), shot blasting, e-coating or painting, as required |
| Inspection | Zeiss CMM (4 units), hardness testers, spectrometer, fluorescent penetrant inspection line |
| Dimensions and tolerances | Per customer 2D/3D drawings |
| Quality system | IATF 16949:2016, ISO 14001:2015 |
Forged Aluminum Bicycle Seat Post Manufacturing Process
- Drawing review and DFM: we confirm alloy, load direction and critical dimensions, then run QForm simulation to predict metal flow and defect risk.
- Die design and manufacturing: the number of die sets (for example, blocker and finisher dies) is planned around part complexity, and die contours are checked with a portable 3D scanner.
- Hot forging: closed-die forming on 600T–8,000T hot forging presses creates a continuous grain flow that follows the part contour.
- Heat treatment: T4 solution treatment and T6 artificial aging are performed in-house, with parameters set by alloy and strength requirement.
- CNC machining and finishing: holes, threads and mating surfaces are machined, followed by deburring, vibratory finishing, shot blasting or anodizing as required.
- Inspection and shipment: dimensions, hardness and chemical composition are verified with CMM, hardness testers and a spectrometer, with lot traceability kept under IATF 16949.
