Drive Shaft Knob-1
Description
Forged Aluminum Drive Shaft Yoke: 3D Forged Yoke for 4WD Drivelines
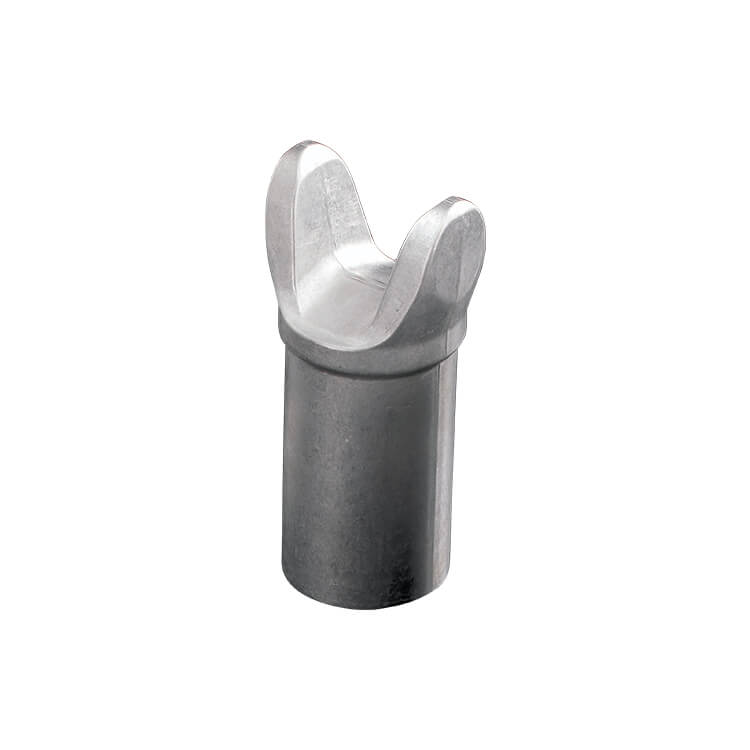
The forged aluminum drive shaft yoke is the fork-shaped joint on a four-wheel-drive (4WD) propeller shaft, 3D hot forged by Al Forge Tech (AFT). Two symmetrical ears at the top carry the universal-joint cross, while the cylindrical body below joins the shaft tube. Ears and body are forged in one piece to carry the torsional and bending loads of the driveline.
A drive shaft yoke sees repeated torque and shock in service, and the root of each ear is a stress concentration. 3D forging distributes grain flow continuously along the ears and body and is less prone to the internal porosity found in castings. AFT completes heat treatment and CNC machining of the ear bearing bores, body diameters and faces, and verifies the coaxiality of the two ear bores on CMM.
Key Features
- 3D forged with continuous grain flow through ears and body
- Designed for 4WD propeller shaft systems
- Ear bearing bores and body fits CNC-finished
- Ear bore coaxiality and position checked on CMM
Forged Aluminum Drive Shaft Yoke Specifications and Manufacturing Capability
| Item | Details |
|---|---|
| Product category | Aluminum Forging Industrial Hardware |
| Application | 4WD vehicle propeller shafts, universal-joint connections |
| Primary process | Closed-die hot forging (hot forging presses 600T–8,000T) |
| Material | Selected to customer specification; 2xxx, 5xxx, 6xxx and 7xxx series aluminum alloys available (e.g. 2014, 6061, 6082, 7075) |
| Heat treatment | In-house T4 solution treatment (8 units) and T6 artificial aging (7 units), set by alloy and strength requirement |
| Secondary machining | CNC machining (52 machining centers, 30 lathes), deburring, vibratory finishing |
| Surface finish | Anodizing (including hard anodizing), shot blasting, e-coating or painting, as required |
| Inspection | Zeiss CMM (4 units), hardness testers, spectrometer, fluorescent penetrant inspection line |
| Dimensions and tolerances | Per customer 2D/3D drawings |
| Quality system | IATF 16949:2016, ISO 14001:2015 |
Forged Aluminum Drive Shaft Yoke Manufacturing Process
- Drawing review and DFM: we confirm alloy, load direction and critical dimensions, then run QForm simulation to predict metal flow and defect risk.
- Die design and manufacturing: the number of die sets (for example, blocker and finisher dies) is planned around part complexity, and die contours are checked with a portable 3D scanner.
- Hot forging: closed-die forming on 600T–8,000T hot forging presses creates a continuous grain flow that follows the part contour.
- Heat treatment: T4 solution treatment and T6 artificial aging are performed in-house, with parameters set by alloy and strength requirement.
- CNC machining and finishing: holes, threads and mating surfaces are machined, followed by deburring, vibratory finishing, shot blasting or anodizing as required.
- Inspection and shipment: dimensions, hardness and chemical composition are verified with CMM, hardness testers and a spectrometer, with lot traceability kept under IATF 16949.
FAQ
What is 3D forging, and why does it suit a drive shaft yoke?
3D forging is closed-die forging in which three-dimensional dies form a complex shape in several directions at once, producing ears, body and transition radii in one operation. Because the yoke ear roots carry torsion and bending, continuous grain flow along the contour gives a more even strength distribution, and the near-net shape reduces subsequent machining.
How is coaxiality of the two ear bores ensured?
The ear bores are usually machined in a single CNC setup after heat treatment, so both bores share one datum and avoid errors from separate operations. Twelve of AFT’s 52 CNC machining centers are 4.5-axis, suited to multi-face work, and coaxiality and position are measured on Zeiss CMM with inspection records retained.
How does a forged aluminum Forged Aluminum Drive Shaft Yoke compare with casting or machining from billet?
Forging shapes aluminum in the solid state under pressure, so the grain flow follows the part contour and the porosity and shrinkage common in castings are avoided. Compared with machining from solid billet, a near-net-shape forging removes less material and shortens machining time. For a Forged Aluminum Drive Shaft Yoke under repeated loads, forging balances strength and weight; the final choice still depends on design loads and volume.
Is heat treatment for the Forged Aluminum Drive Shaft Yoke done in-house?
Yes. Al Forge Tech operates 8 T4 solution treatment units and 7 T6 artificial aging units on site, so the Forged Aluminum Drive Shaft Yoke can be solution treated, quenched and aged in the same facility before machining and inspection. Keeping heat treatment in-house removes inter-plant transport, reduces lead-time risk and keeps lot traceability within one quality system. Parameters are set according to the alloy grade and your specification.
How do you keep the Forged Aluminum Drive Shaft Yoke consistent from lot to lot?
Al Forge Tech runs incoming (IQC), in-process (IPQC) and final (FQC) inspection under IATF 16949:2016, supported by 4 Zeiss CMMs, hardness testers, a spectrometer and a fluorescent penetrant inspection line. First, middle and last pieces of every lot are checked against the die; when wear causes dimensional drift, the die is reworked to keep the Forged Aluminum Drive Shaft Yoke stable across lots.
Request a Quote for the Forged Aluminum Drive Shaft Yoke
Developing a new Forged Aluminum Drive Shaft Yoke or converting an existing part to aluminum forging? Send us your 3D/2D drawings, alloy and temper, annual volume and finishing requirements. Our engineering team will reply with a feasibility review, die plan and quotation.
- Online inquiry: Contact Us
- Email: [email protected]
To compare similar parts, browse Aluminum Forging Industrial Hardware and our industrial hardware forging applications, or visit About Us for our equipment and certifications.
